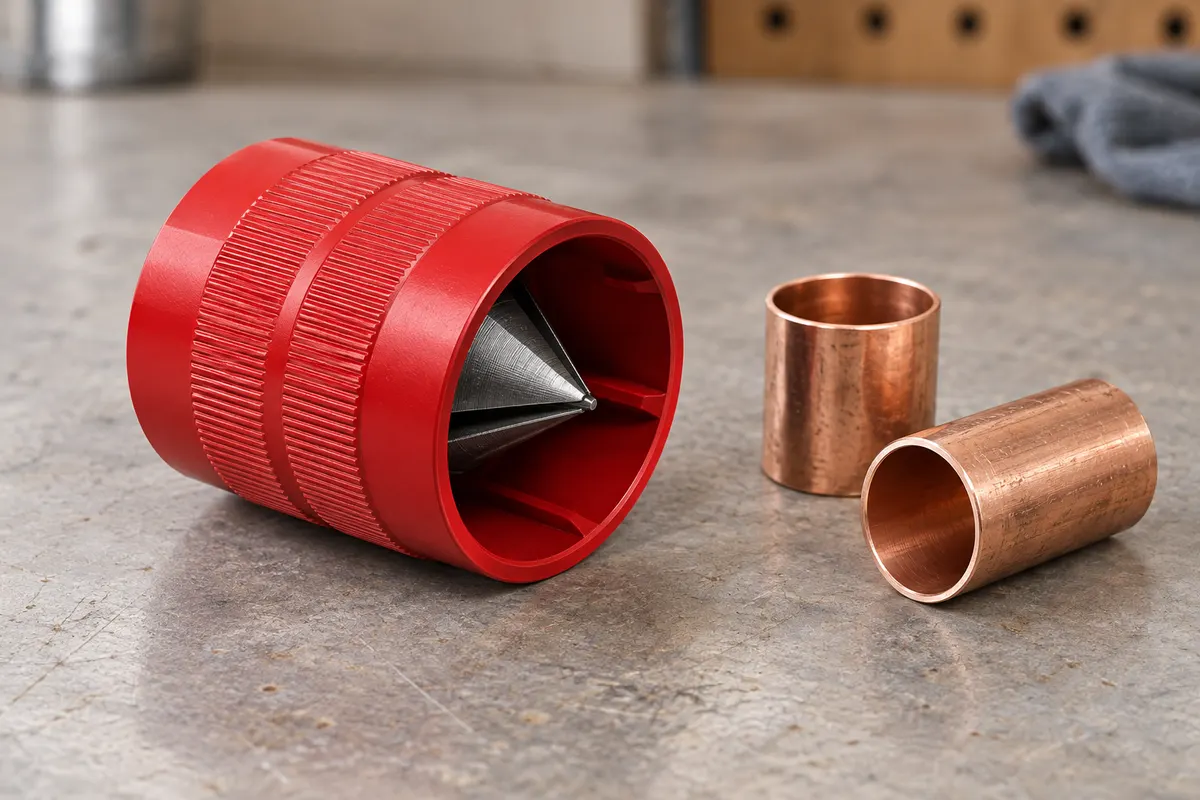
A REPEATABLE METHOD
How to use it
- Read the fitting-system preparation requirements. Identify whether it needs deburring, chamfering, calibration or a dedicated combined tool.
- Check material and diameter capacity of the reamer. Work with a loose, cool and securely supported tube end.
- Inspect the cut for squareness and crushing. Correct an unsuitable cut before removing burrs.
- Use the appropriate inner or outer cutting end with gentle controlled turns according to its manual. Remove the burr, not a large ring of sound wall.
- Inspect visually under good light, collect chips and clean by the system’s method. Recheck dimensions and required insertion preparation before joining.
INTERPRET THE MEASUREMENT
How to read the result
- A smooth-looking outside edge does not prove the inside burr has gone.
- The required chamfer comes from the connection instructions; a cone does not define a universal angle or depth.
- Do not rub a fingertip around a sharp pipe end to judge the result. Use light and appropriate inspection tools.
Work through an example
Illustrative situations and readings, not product tolerances. Follow the instructions for your own tool.
A tidy outer edge does not mean the inner burr is goneOpen the worked exampleClose the worked example
A compatible deburring tool is tried on a supported, loose tube offcut. After a light preparation pass, the outside looks clean but an inner burr remains visible. These are fictional visual observations.
Before you start
- Match the tool to the material and diameter and read the fitting preparation requirements.
- Secure the loose offcut and keep hands away from sharp edges and cutting surfaces.
- Inspect inner and outer edges separately under good light; do not check by wiping a finger across the edge.
Example notes
- Outer edge
- Visible burr removed
- Inner edge
- Burr remains visible
- Inside the sample
- Loose chips need removal
What this tells you
Only one edge has been addressed. Visual smoothness outside cannot certify inner preparation, correct dimensions or a leak-free joint. Removing excessive material can also change the required fitting geometry.
Your next step
Complete only the preparation allowed by the tube and fitting instructions, remove loose debris and inspect again. If the end is damaged or the required shape is uncertain, stop and obtain the system instructions.
Do not conclude: Do not keep enlarging the bore until it looks polished or invent a universal chamfer angle or depth.
Method reference: RIDGID: inner and outer tube preparation
TROUBLESHOOT THE METHOD
Common problems and what to check
Tool chatters or catches
Check diameter, material, support and cutting edge. Do not solve incompatibility with more force.
End becomes visibly thin or oversized
Stop and reject the damaged end for the fitting. Recut only if there is enough sound length.
Debris remains inside
Remove and account for chips before connection; follow the system cleaning and flushing procedure.
STOP BEFORE THE HAZARD
Safety boundary
- Keep hands clear of the cutting cone; protect eyes from chips.
- Use only on isolated loose material, not a pressurized installed service.
- Do not substitute a general reamer for a mandatory pipe-system calibration tool.
SMART BUYING GUIDE
What to look for when choosing
- Match the actual material and diameter range.
- Choose a tool that reaches both required edges and can be cleaned and inspected.
Types of tool
Best for: Compatible metal tube ends needing both burrs removed.
Best for: Plastic or multilayer systems that explicitly specify it; not interchangeable with a generic cone.
Common functions
Worth paying more for
- Correct cutter material, capacity and replaceable parts.
- A grip and cutting edges that allow controlled light pressure.
Usually not worth the extra cost
- A promised one-tool replacement for every pipe-system preparation step.
- Aggressive cutters chosen to enlarge the bore.
Sources & instructions
AI-generated topic illustration; do not use the depicted scale for measurements.