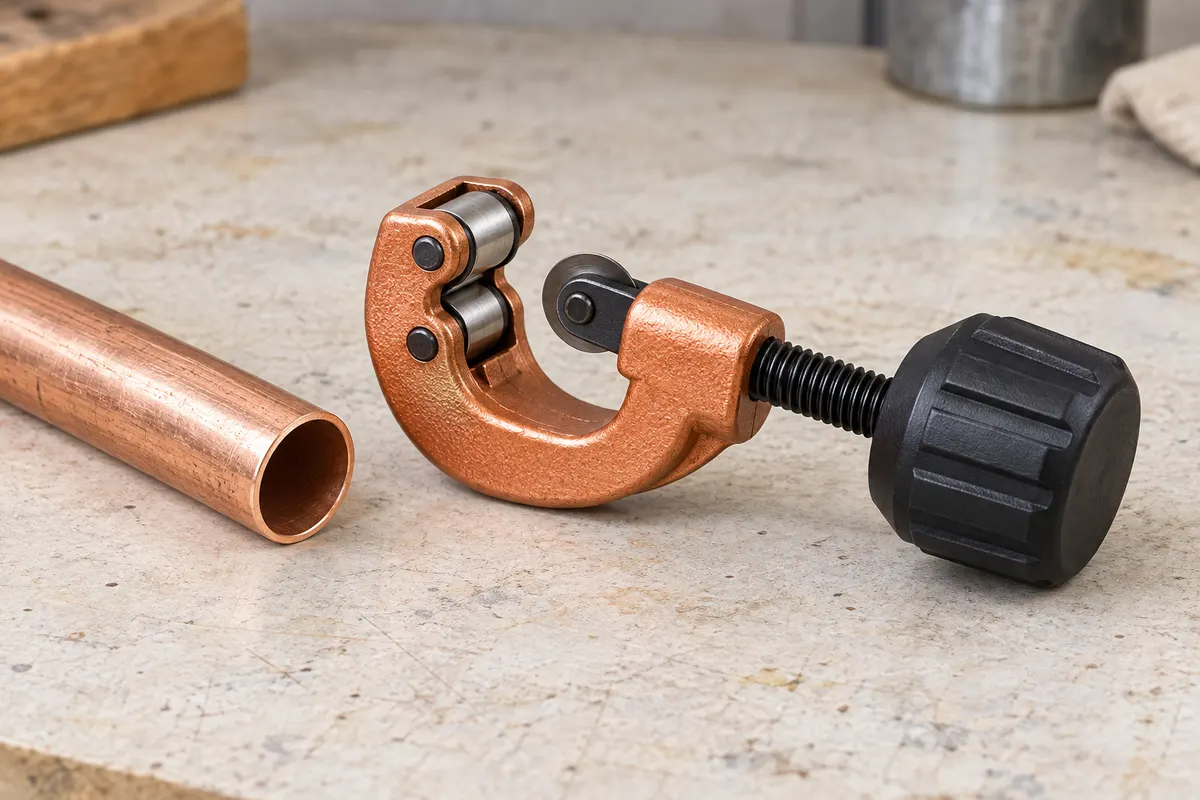
A REPEATABLE METHOD
How to use it
- Identify the tube material, outside diameter and wall thickness. Choose the specific cutter and wheel approved for them.
- Work on a loose, drained, cool piece of tube. System isolation and any gas, refrigerant or regulated installation belong to a competent specialist.
- Measure the finished length with the fitting insertion requirements accounted for separately. Mark the intended cut and support the tube.
- Seat the rollers and wheel squarely. Rotate with the manufacturer’s incremental feed; do not crush the tube by tightening fully at the start.
- Inspect the end for spiral tracking, distortion and burrs. Deburr and clean as the connection system requires; verify the final length before assembly.
INTERPRET THE MEASUREMENT
How to read the result
- Outside diameter selects cutter fit; inside diameter belongs in the water-volume calculator. They are not interchangeable.
- A spiral track indicates movement or misalignment, not an acceptable square end.
- The cut end is only one preparation step. A clean cut does not certify a leak-free connection or completed pressure test.
Work through an example
Illustrative situations and readings, not product tolerances. Follow the instructions for your own tool.
A clean-looking cut can still leave the piece too shortOpen the worked exampleClose the worked example
A loose, cool copper practice tube is cut for a fictional end-to-end length of 120 mm. It is not attached to a service, contains no fluid and is not pressurised. After cutting, the measured length is 119 mm.
Before you start
- Check that the cutter and wheel suit the actual tube material and outside diameter.
- Support the loose sample and mark the required finished endpoints, including any fitting allowances in the plan.
- Use the cutter instructions and remeasure the finished piece from the same reference.
Example notes
- Planned sample length
- 120 mm
- Measured finished length
- 119 mm
- Cut edges
- Still require inspection and preparation
What this tells you
The measured piece is 1 mm shorter than the fictional plan. This is a length comparison, not a universal rejection tolerance. A neat edge does not confirm the required fitting engagement or readiness for assembly.
Your next step
Check the measurement and actual joint requirements before deciding whether the piece is usable. If it cannot meet the plan, prepare a new sample. Inspect and prepare both edges by the tube and fitting instructions.
Do not conclude: Do not compensate by reducing required fitting engagement, and never use this practice example as instructions for cutting an installed or pressurised line.
Method reference: RIDGID: material-specific tubing cutters
TROUBLESHOOT THE METHOD
Common problems and what to check
Tube end is flattened
Stop. Check wheel, material suitability and feed. Remove the damaged section only if the final length still works.
Two grooves or a spiral
Recheck squareness, support and wheel condition on a spare piece before continuing.
Cutter will not rotate in the space
Use an approved close-quarters tool or prepare loose tube at the bench. Do not remove guards or improvise system access.
STOP BEFORE THE HAZARD
Safety boundary
- Never cut an unknown, pressurized, hot or connected live service.
- Protect eyes from chips; support both resulting pieces and keep hands clear of the wheel.
- Collect metal debris. Do not leave swarf inside drinking-water piping.
SMART BUYING GUIDE
What to look for when choosing
- Match material and wall thickness, not only the largest diameter printed on the box.
- Check replacement wheel availability and the room needed for rotation.
Types of tool
Best for: Loose compatible tube with access around the full circumference.
Best for: Compatible tube where the tool’s approved operating space is restricted.
Common functions
Worth paying more for
- Correct replaceable wheel and stable rollers.
- Smooth feed without play.
Usually not worth the extra cost
- Universal-material claims unsupported by the wheel specification.
- Capacity you cannot rotate around the tube.
Sources & instructions
AI-generated topic illustration; do not use the depicted scale for measurements.